Precast construction turns a building site into an assembly yard. Columns, beams and slabs are cast in a factory while the foundations are being dug, and then erected in days. But a precast frame is only as good as its joints, and the most important joint of all is where the column meets the foundation.
In this paper, Dr. N. Subramanian reviews the five main ways of connecting a precast column to its foundation and sets out a design method based on the new Eurocode 2 (BS EN 1992-1-1:2023), because the Indian code IS 15916:2010 gives very little guidance on column-foundation connections. Below is a summary of the key ideas, design equations and detailing rules from the paper.
Why precast, and why the connection matters
Factory casting gives better quality control (indoor curing, steel moulds, batch testing), parallel working on site and in the factory, faster erection, less formwork waste and less site noise and dust. Prestressing allows long spans and fewer columns.
However, a precast frame does not behave like a monolithic cast-in-situ frame. Continuity is not automatic. The designer must clearly identify where the forces come from, how they travel through each component, and how they are safely passed through the connections into the foundation.
Five ways to connect a precast column to its foundation
- Pad foundation with a separate smooth-sided pocket cast on top. The traditional approach, now largely replaced.
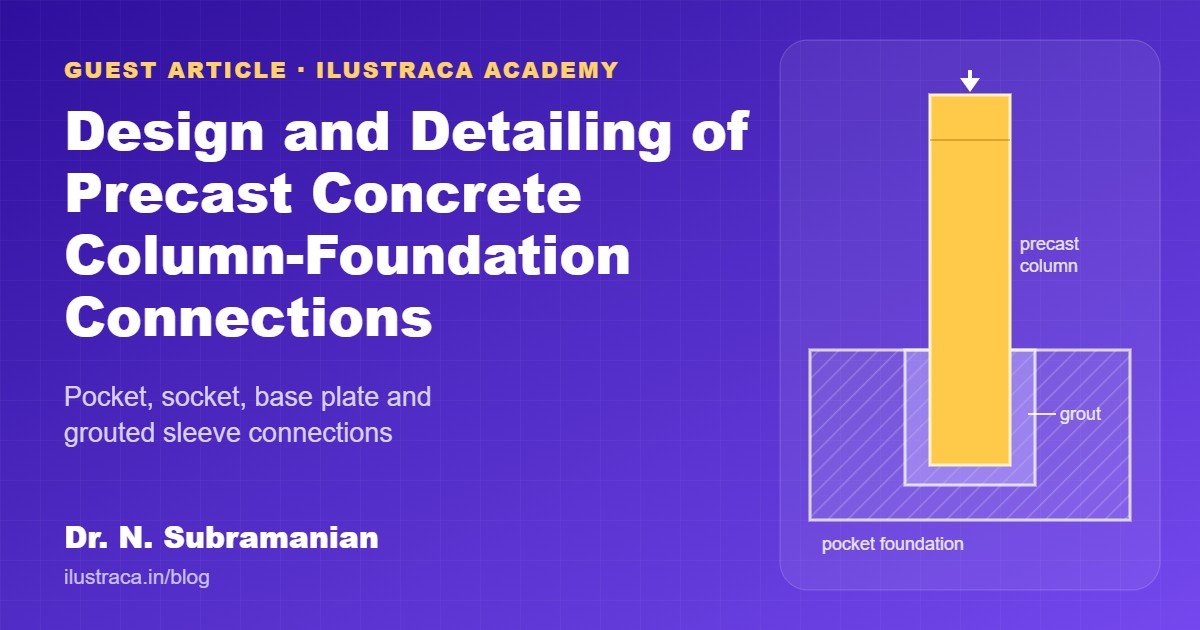
- Integrated pocket foundation, with the pocket formed directly in the foundation block. More economical, allows shallower foundations and larger erection tolerances. The pocket walls can be smooth or keyed.
- Monolithic precast column-foundation unit, cast as one element in the factory, placed on a blinding layer, levelled with steel shims and grouted underneath (with vertical grout pipes to avoid air pockets). Fast, but heavy to transport; road limits usually cap the base width at about 3 m.
- Steel base plate on holding-down (anchor) bolts, popular in the USA and Germany. Levelling nuts allow precise alignment and the column is stable immediately, but it is the most expensive option.
- Columns on grouted sleeves: starter bars from the foundation enter corrugated steel sleeves cast in the column, and the annulus is filled with expansive grout. One of the most widely used and economical connections.
Practical rules for pocket foundations
- The annular gap between column and pocket should be at least 50 mm at the bottom and 75 mm at the top.
- Fill it with non-shrink concrete (minimum M30) or, more often, a 2:1 non-shrink grout (coarse sand up to 6 mm and cement) that reaches about 20 N/mm² in 2–3 days, so props and wedges can be removed early. The in-situ foundation is usually M25/M30.
- The column needs a good “key” with the pocket for skin friction: profiled column bases (trapezoidal battens in the mould), a retarder to expose the aggregate, or permanent corrugated sheet-metal pocket formers.
- Provide bursting links at the column base: about 2–3 links of 10 mm diameter at 50 mm spacing.
- Where column bars are in tension, they must be fully anchored in the pocket; hooks or bends keep the pocket depth manageable.
Columns on grouted sleeves
- A nominal annulus of 6 mm is standard. If it is wider (about 25 mm), gravity grouting works; otherwise pressure grouting is needed.
- Grout strength should match the column, typically at least 40 N/mm².
- Corrugated pressed-steel sleeves (about 1 mm thick) wedge into the concrete and can stay in place; smooth sleeves must be withdrawn.
- Columns are levelled on packing shims (fixing tolerance about 40 mm) and stay propped until the grout hardens and the first floor beams and slabs are in.
- Because the starter bars sit in the column corners, the main bars move inwards. The effective depth is roughly d ≈ h − 110 mm.
- Full-scale tests (Hofer et al. 2021, Kuttab et al. 1988) show axial force-moment interaction, ductility and energy dissipation similar to cast-in-place columns.
Designing a pocket foundation to Eurocode 2:2023
With a smooth pocket, the vertical force goes straight to the base of the column, which needs at least 300 mm of concrete below it. The infill grout strength is typically 30 N/mm². Two failure modes govern:
- Diagonal tension shear across the corners of the pocket. Provide links around the top half of the pocket.
- Crushing of the annulus. The ultimate bearing stress is limited to 0.482 fcki, applied conservatively over the column width only.
With a rough or keyed pocket, vertical load and moment are carried by shear friction at the interface. The coefficient of friction μ from Table 8.2 of BS EN 1992-1-1:2023 depends on the surface:
| Surface | Description | μ |
|---|---|---|
| Very smooth | Cast against steel, plastic or specially prepared timber moulds | 0.5 |
| Smooth | Less than 3 mm roughness, e.g. a free surface left after compaction | 0.6 |
| Rough | At least 3 mm roughness (raking or exposed aggregate, max 40 mm spacing) | 0.7 |
| Very rough | At least 6 mm roughness | 0.9 |
| Keyed | Surface with shear keys (0.5 ≤ h₁/h₂ ≤ 2.0) | 0.9 |
Embedment length
- l ≥ 1.2h when M/Fv ≤ 0.15h
- l ≥ 2.0h when M/Fv ≥ 2.0h
- Interpolate between these limits (h = larger side of the column).
Equilibrium of the column in the pocket
Moment and shear are resisted by a couple of horizontal compressive forces F1 (near the top) and F2 (near the bottom), assumed to act 0.1l from the top and bottom of the pocket, plus the base reaction F3 and the friction forces μF1, μF2, μF3:
Horizontal: Fh = F1 − F2 − μF3
Vertical: Fv = μF1 − μF2 + F3
Moments about F2: 0.9Fhl + M + 0.5Fvh − F3(0.5h − 0.1μl) = F1(0.8l + μh)
which gives F3 = (Fv − μFh) / (1 + μ²), and then F1 and F2.
The checks that follow:
- Grout: √(F3² + (μF3)²) ≤ 0.482 fck b h, and required grout strength fck ≥ F1 / 0.482b.
- Foundation concrete under the infill: fck(i) ≥ F1 / 0.482bp, where bp = b + 2 × annulus.
- Links at the top of the pocket: Ash = F1 / 0.87fy. With a pocket taper θ of 3°–5°, Ash = (F1 − μFv tanθ) / 0.87fy and F3 = (Fv − 2μFv tanθ − μFh) / (1 + μ²).
- Use several small links (three to six 8–12 mm bars) rather than a few large ones, to keep bend radii small.
- Compression strut in the side walls: Fc = √2·F1, strut width w = √2·F1 / (0.482 fck(i) t) ≤ 0.5l.
- Edge distance at the top of the pocket: 0.5F1 ≤ τc × 0.2l × df.
Anchorage, depth and detailing
- Column bars extend at least one design anchorage length lbd (typically 38φ), starting 50 mm below the top of the pocket. The length may be reduced pro rata where As,prov exceeds As,req.
- Hooks or bends can cut the required anchorage depth by about 50%. The bond length must never be less than 12φ.
- The method is for uniaxial bending. For biaxial bending, use an equivalent increased uniaxial moment in the critical direction.
- Plinth depth is usually taken equal to the column dimension, capped at 400 mm. Check punching shear for the temporary stage before the infill hardens.
- Load spreads at 45°–60° from the column edge. For 45°, the required depth is about D = (H − h)/2.
Pocket foundations with shear keys
Keyed pockets aim for true monolithic behaviour, with the column bars lapping the foundation starters through strut-and-tie action. The embedment is l = lsd + s, where lsd = 1.5 ld (Clause 13.8.2 of BS EN 1992-1-1:2023) and s, the distance between lapped bars, is usually 130–170 mm.
For fy = 415 N/mm² and fck = 30 N/mm², l ≈ 57φ + 150 mm, which means about 1575 mm for 25 mm bars and 1975 mm for 32 mm bars. These depths are impractical with straight bars, so hooks or bends and links around the pocket perimeter are needed.
Columns in pedestal socket foundations
- A base slab with a thickened central pedestal containing a rectangular or circular socket. Pedestal walls are thin (about 175–200 mm) and need careful detailing.
- Loads pass by side shear and base bearing, with passive pressure on the socket walls resisting overturning.
- Socket connections can give 7.5% to 51% higher peak horizontal force capacity than cast-in-place piers, though with slightly lower displacement capacity (Hemamathi et al., 2026).
- Embedment of 0.8 to 1.0 times the column dimension is recommended for seismic performance comparable to cast-in-place. Osanai et al. (1996) found that 1.5h or more behaves as rigid even without shear keys, and Jiang et al. (2024) identified about 0.7D as an optimal balance.
- Reinforcement: vertical and horizontal bars in each wall tied at the corners, extra stirrups over 300 mm at the column base for bursting, secondary steel at wall mid-spans, and wall steel lapped into the base slab.
Seismic and impact performance
Research summarised in the paper shows that well-detailed pocket connections, especially fully embedded or keyed ones, can match or exceed monolithic connections in ductility, energy dissipation and strength. Socket and pocket connections also resist vehicle impact well when the horizontal steel in the top half of the pocket is increased and the infill grout is stronger than the surrounding concrete.
Key conclusions
- The coefficient of friction strongly affects force transfer: from 0.5 for very smooth to 0.9 for keyed or very rough surfaces.
- Adequate embedment, typically 1.2h to 2.0h depending on M/Fv, prevents pull-out and ensures moment transfer.
- Links in the top half of the pocket and bursting reinforcement at the column base prevent diagonal tension and crushing failures.
- Integrated pocket foundations and grouted sleeves are efficient and economical. The final choice depends on soil, transport and assembly speed.
- Precast connections such as grouted sleeves and keyed pocket foundations can achieve seismic performance comparable to, or better than, monolithic cast-in-place connections.